
 BBELC
Procuring High-Quality Power Transformers
The parameters listed on the quotation often appear to be flawless, and suppliers can easily produce several high-quality product images along with a “compliant” test report. But this instead makes it difficult for the purchasing staff-which equipment is really reliable? In fact, the crux of the problem is often not that you missed a certain eye-catching publicity indicators, but that we did not take the “quality” of the word, disassembled into visible, tangible hard evidence.
When our purchase order specifies the need to buy “high-quality power transformers,” it is by no means the adjective “high-quality” that ultimately matters. The key point is: whether the matching degree of this equipment with the actual system is enough? Is the manufacturing process strictly controlled? Is the test data actually specific to the machine you bought? And whether the technical documents attached to the delivery can provide real support for the later installation and maintenance.
Quantify the Word “Good” into Specific Acceptance Criteria
Before sending out the request for quotation, be sure to finalize all the details. For example, primary and secondary rated voltage, frequency, phase number, grounding mode, voltage deviation, as well as specific working conditions of continuous load and short-term operation. If there is a motor, rectifier or inverter in the load, the current waveform, harmonics, load cycle, peak value and demand coefficient must also be clearly written in. If these prerequisite conditions are not clearly specified, even with the same “rated capacity,” the actual thermal load and insulation requirements that the equipment must withstand can differ dramatically.
When it comes to environmental conditions, never just dismiss it with a simple “indoor” or “outdoor.” Temperature, altitude, humidity, whether there will be condensation, dust, there is no corrosion, as well as ventilation path, installation space and transportation restrictions… These will directly affect the equipment insulation system, cooling mode, shell design and mechanical structure. These details must be explicitly documented in the technical agreement so that there is a consistent benchmark for subsequent design and acceptance.
When comparing prices, don’t just focus on terms like “low loss,” “low noise,” or “high efficiency.” To know, only in the reference temperature, load point, cooling conditions and measurement environment are exactly the same premise, to compare the loss, efficiency, temperature rise and noise level has practical significance.
Carefully Review Whether the Design Truly Matches the Load
Just because a general-purpose product can handle the load doesn’t mean it’s necessarily suitable for your specific system. Take the phase-shifting rectifier transformer as an example, the number of bridge groups, the number of pulse waves, the phase-shifting angle, the voltage and current on the valve side, the impedance between the windings, and the unbalance of the load are all used as input parameters for the design. Be aware that non-sinusoidal currents change the losses and hottest spot temperatures in the windings, cores, clamps, and leads. Therefore, when performing thermal design, one must never take shortcuts by directly applying standard sine-wave current ratings.
For example, Shanghai North Transformer (Shanghai North Transformer) can deeply customize the capacity, voltage, number of windings, phase shift angle, impedance, insulation level, cooling method, and even the shell and installation method of the transformer according to the project requirements. When evaluating the plan, the procurement team should focus on how these customized options fit our system architecture, load characteristics and site environment, rather than simply counting the number of models listed in the product catalog.
If multiple devices are operating in parallel, the transformation ratio, connection group, phase shift, impedance percentage, tap position and manufacturing tolerance must be carefully checked. Don’t ever assume that just because the mechanical interfaces fit perfectly, the electrical loads will necessarily be distributed evenly.
Process Records Are Much More Convincing Than Workshop Photos
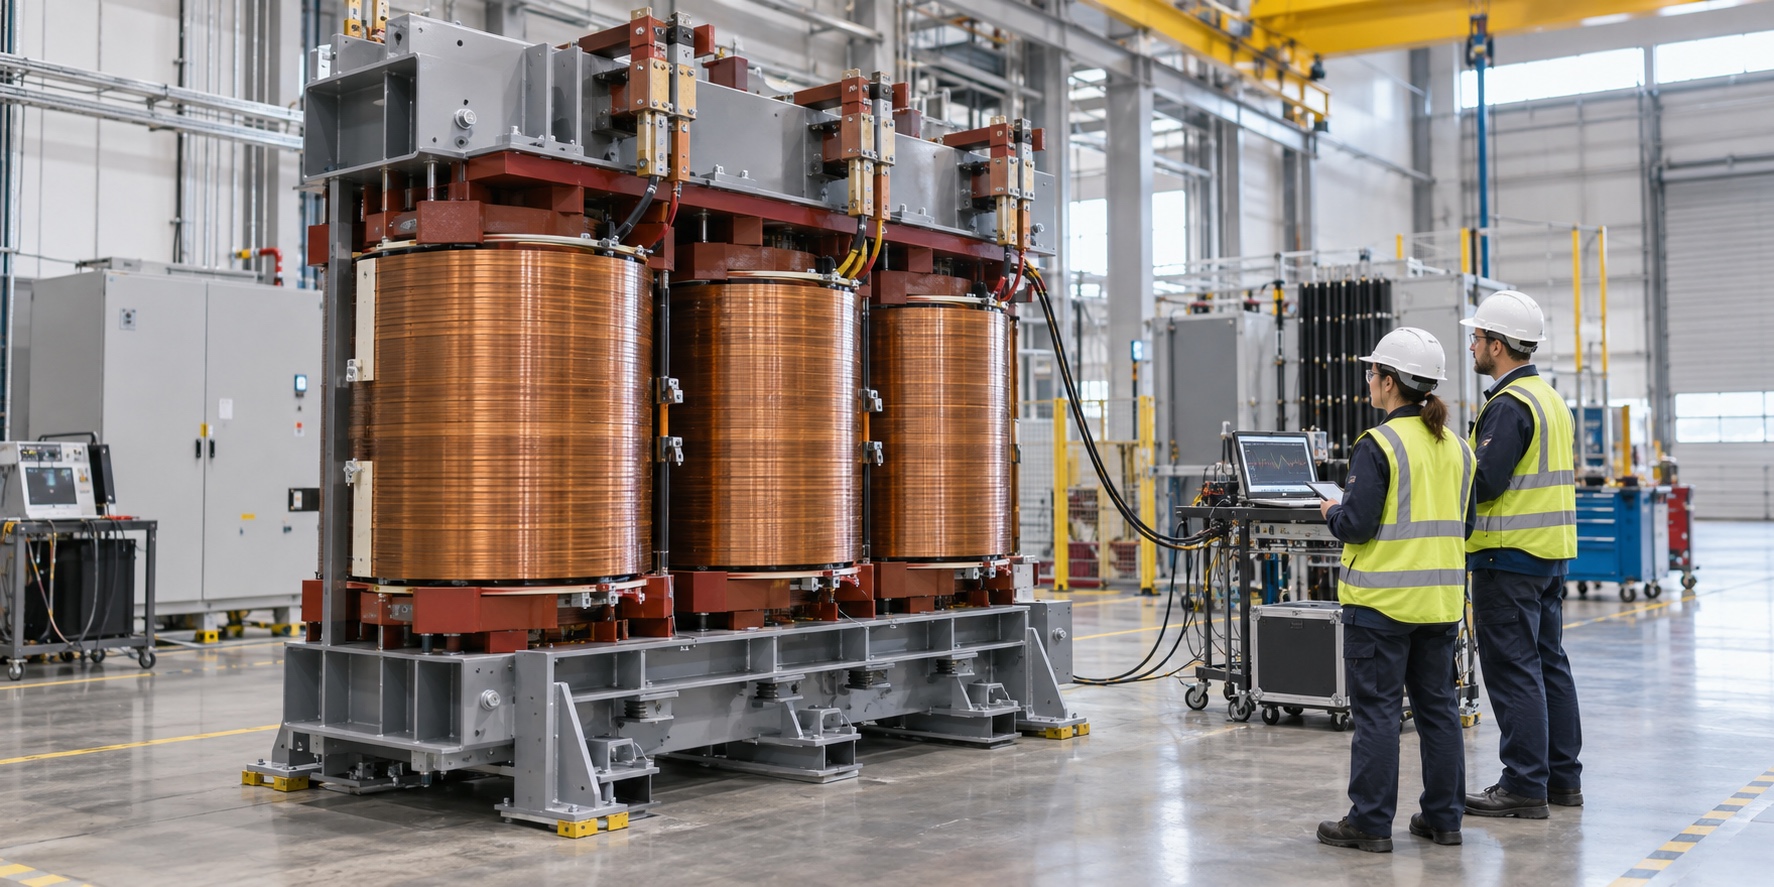
Product quality is by no means finalized only at the final finished-product inspection stage. Take the dry-type rectifier transformer as an example, from the material entering the factory, winding, dipping paint, to the processing of insulating parts, the stacking of iron cores and the final assembly, every link can be checked and tested. Raw and auxiliary materials such as bare electromagnetic wire, insulating paper, insulating paint, silicon steel sheet and clip must be inspected before warehousing. However, the steps of winding, welding, dipping paint or pouring, curing and assembly must strictly control various process parameters in place.
When you go to the site for inspection, you may as well conduct a “reverse spot check” on the orders being produced: see if the key materials can be traced back to the specific batch; Can the process record match the unique identification of the product? Are all measuring instruments within the validity period? How were those unqualified products isolated, processed and re-inspected? There are also design changes, whether they have been truly implemented on the final drawings. At best, a clean and tidy workshop can leave you a good visual impression. What can really reflect the level of process control is a complete chain of records that cannot be dropped.
Carefully Review the Test Report; Don’t Just Settle for a Simple “Pass” Mark
Conventional tests generally include winding DC resistance, voltage ratio and phase relationship, short-circuit impedance, no-load and load losses, insulation resistance, external voltage withstand, induced voltage withstand, and partial discharge tests. Each test item has a different focus. For example, the transformation ratio and phase angle test are to verify whether the number of turns and the connection group of windings are correct. The loss test looks at the performance related to the iron core or winding. Furthermore, the insulation stress evaluated in withstand voltage and partial discharge tests is entirely different from that assessed in other tests. Therefore, one must never use the results of one test to replace or obscure the results of another.
1 a formal report, which should include sample identification, model, capacity, winding configuration, voltage, tap location, frequency, environmental conditions, test methods and equipment, as well as measured values, allowable ranges and final conclusions. No matter which phase, which tap position or which winding measures the data, the original records must be meticulously written down and preserved. The data obtained under different temperatures, tap positions, load levels or test configurations must not be directly compared without conversion and standardization, otherwise it is very easy to draw wrong conclusions.
Before doing the factory acceptance test (FAT), it is best to arrange the test items, wiring methods, acceptance criteria, witness process, and the response plan in case of a situation in advance. If the test fails, don’t worry, first analyze the cause and scope of influence, and then finalize the maintenance plan, design changes and the scope of retesting.
Figure Out What This Report Can Actually Prove
Routine testing (I. e., factory testing) is to verify that each machine is manufactured in accordance with basic consistency; type testing is used to test that the regulatory performance of a particular design is not up to standard; as for special testing, it depends on the project The specific agreement. Each of these three tests has its own purpose. Don’t take a single prototype or a specific model of the qualified report, of course, applied to other products with different capacity, voltage, insulation structure or material combination.
For certifications and various reports, their scope of applicability must also be carefully verified. Who is the certificate holder, the place of manufacture, the specific model or series, the standard version to be followed, the validity period, and the supervision conditions all match the current order. Everyone must be clear: a quality management system certificate, only that the factory’s management system has passed the audit, it can never replace the specific product type test, factory acceptance test or project acceptance.
Before Shipment, Conduct a Final Closed-Loop Verification.
After the electrical tests have passed successfully, don’t forget to check the nameplate, final drawings, terminal identification, accessories, spare parts, cooling and temperature control functions, transportation fixtures and packing list. Even if only a few small package accessories are missing, or if there is something wrong with the interface and logo, the progress of Yan ‘an installation and debugging will be dragged down on the spot.
At the end of the day, we might as well ask the supplier a core question directly: from the initial input of the project, the approval of design drawings, the batch of materials, the key process flow, to the original data of the factory, so many ring energy can’t be traced back completely and smoothly on the same equipment? If this traceability chain is broken at any link, then when the acceptance conclusion is drawn, we must not rush to label this product as “high quality.