
 BBELC
How to Evaluate a Rectifier Transformer Manufacturer
When you get several quotations for rectifier transformers, the most easy to compare is the price, capacity and delivery period. What is really easy to be missed is the rectifier interface. The rated capacity of the two devices seems to be close. As long as the number of bridge groups, pulse wave number, phase shift angle, impedance matching or operating conditions are different, they cannot be judged on the same reference line.
When choosing a rectifier transformer manufacturer, don’t rush to look at the factory’s size or product catalog. The comparison is meaningful only if the system conditions are clearly written and each candidate is required to answer the same set of questions with design documents, test plans and deviation tables.
First, See Whether the Manufacturer Has Asked the Right Question
A rectifier transformer is not simply a general-purpose transformer with several low-voltage windings added. It is not only to complete the voltage conversion and electrical isolation, but also to the multi-pulse rectifier circuit to provide multiple sets of phase difference of low-voltage power supply. At the beginning of the program, the manufacturer should at least ask about the rectifier type, the number of bridge groups, the number of pulse waves, the DC voltage and current range, the operating quadrant, and the phase shift and impedance requirements of each winding.
The project party shall also provide the rated voltage and allowable deviation, frequency, short circuit capacity, grounding mode, background harmonics and common connection point limits of the AC system. The load side should not only give a total power figure, but also indicate the DC load, duty cycle, overload period, trigger mode, allowable DC ripple, normal, low load, single bridge shutdown and grid imbalance at each operating point.
If a candidate only quickly recommends standard models based on capacity and primary voltage, but does not confirm these interface conditions, the following temperature rise, average current and harmonic judgments lack a reliable starting point.
Ledging Product Capabilities to Current Project
Just because a manufacturer has showcased high-capacity products doesn’t mean they can directly implement your solution. When checking, we should look for design experience close to the voltage, capacity, winding structure and load characteristics of this project, and see if it can handle the really difficult part of the current project.
For example, a multi-winding phase-shifting rectifier product may need to convert the primary side voltage into multiple sets of phase-difference low-voltage outputs; a four-quadrant system also involves bidirectional energy flow; and a data center front end may face multiple independent rectifier modules. Impedance is not the larger or smaller the better, it is to limit the short-circuit and phase change current, maintain DC voltage, control harmonics and bridge group to achieve a balance between the current.
When checking the design input, the capacity, voltage, number of windings, phase shift angle, impedance, insulation level, cooling method, enclosure protection level, installation size and environmental conditions shall be listed in the technical agreement one by one. Installation space, altitude, humidity, dust or corrosive environment will change the insulation, cooling and structure selection, and can not wait for the drawings to freeze before filling.
When Visiting a Factory, Observe the Process, Not Just the Finished Product.
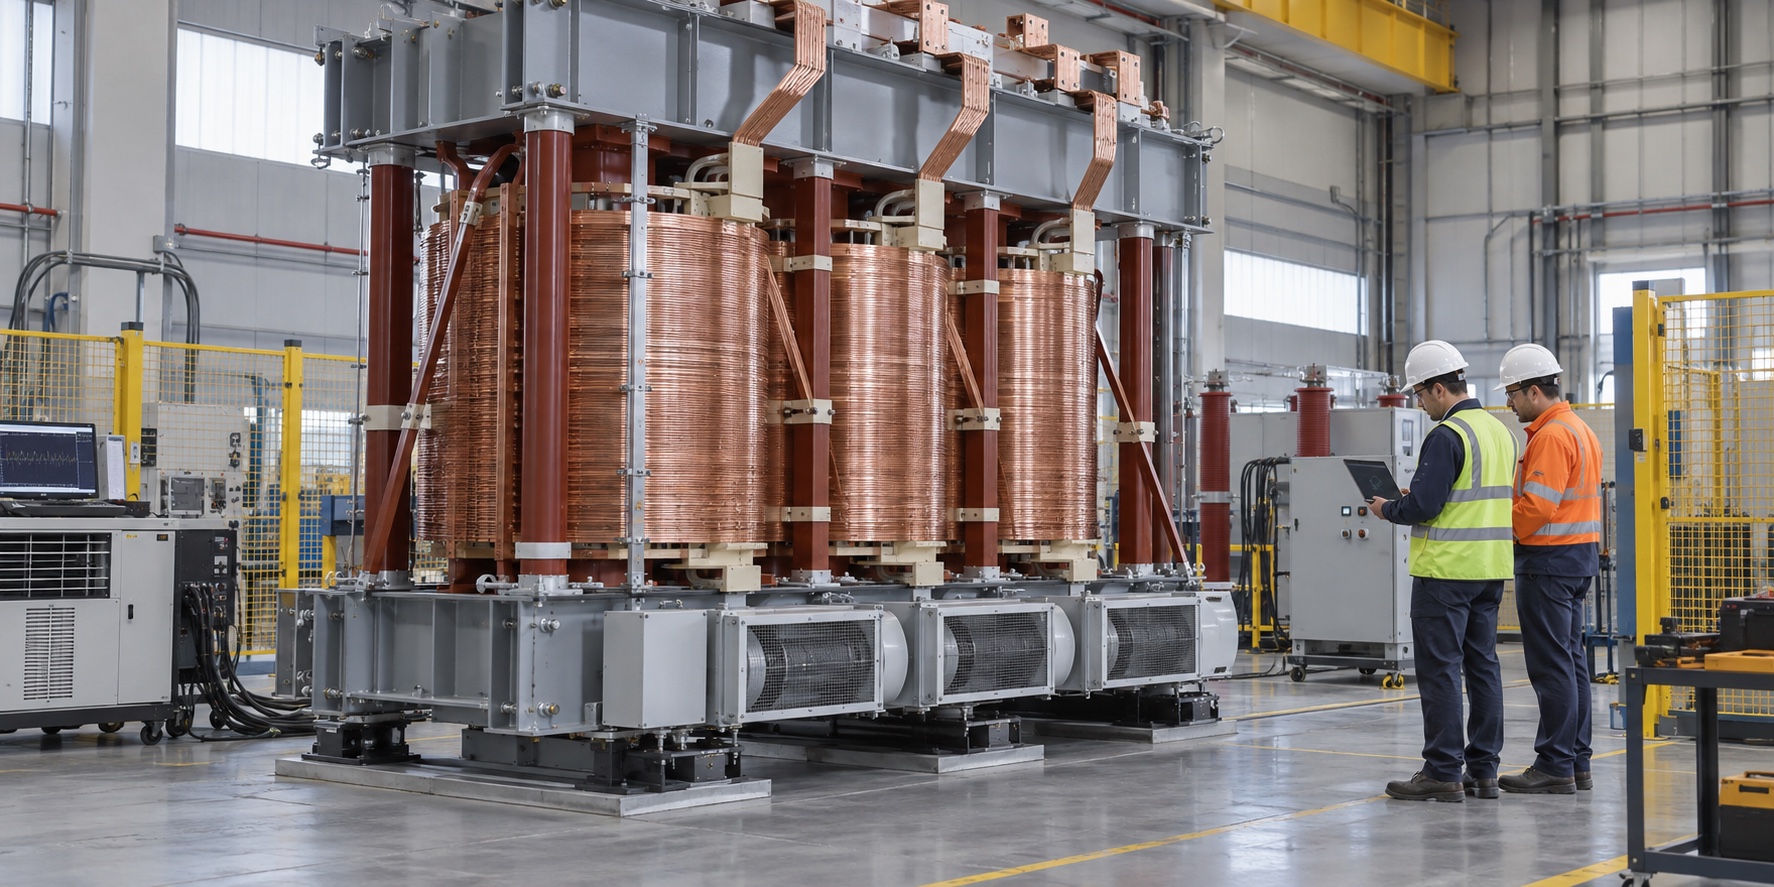
The focus of the factory audit shall be whether the coil, insulation treatment, core, assembly and test form a continuous quality chain. The manufacture of dry-type rectifier transformers usually proceeds from contract review into product design and production planning, followed by material procurement, incoming inspection, component manufacturing, final assembly, finished product testing and factory inspection. Raw and auxiliary materials such as bare magnet wire, insulating paper, insulating paint, silicon steel sheet and clip shall have inspection records before warehousing.
Then conduct spot checks based on actual orders. Whether the coil winding, welding, dipping or curing leave process records, whether the iron core is cut and stacked without semi-finished products for inspection, how to approve the design change, how to isolate the unqualified products, and whether the measuring instrument is in the calibration state. The factory floor area and the model area are very straightforward, but they cannot replace this traceable evidence.
Also ask which processes are made by the factory and which rely on outsourcing or outsourcing. Approved suppliers, substitution rules and inspection responsibilities of key accessories should state that the manufacturing capacity of the host cannot automatically prove that all purchased parts are equally controlled.
Validate the Quotation Commitment Using a Pilot Program
The loss, efficiency, temperature rise, impedance and partial discharge data in the technical quotation can only be compared when the test conditions and scope of application are clear. Figures for different products, different cooling conditions or different environmental benchmarks cannot be directly listed in one table to draw high and low conclusions.
The finished product test of the rectifier transformer can cover the appearance, insulation resistance, voltage ratio and phase shift angle, winding resistance, short-circuit impedance, load loss, no-load current, no-load loss, applied voltage withstand, induced voltage withstand and partial discharge measurement. Routine tests, type tests, special tests, witness points, acceptance criteria and original record delivery scope shall be agreed in advance in the procurement documents, instead of receiving only one "OK" conclusion after the equipment is completed.
In particular, confirm how the phase shift angle, the impedance matching of each LV winding and the bridge group interface are verified. 12 pulse wave system requires two sets of secondary voltage, 30 electrical angle phase shift, impedance matching, bridge group series and parallel connection and load balancing. When the pulse wave number is higher, rectifier supplier, transformer manufacturer and system designer also need to jointly confirm phasor, connection group, phase sequence, bridge group number and protection logic.
Finally, Compare the Scope of Responsibilities and Delivery Capabilities.
After technical qualification, then compare prices and delivery times. Get all candidates to submit an item-by-item compliance matrix, separating compliance, deviation, to be clarified, and not applicable; key deviations cannot be obscured by the total score or low price. The quotation should also be adjusted to the same scope of supply, including testing, documentation, packaging, transportation, spare parts and interface responsibilities with the rectifier.
The delivery period shall be broken down into traceable milestones: drawing approval, design review, material locking, manufacturing, witness testing, shipment approval and transportation to the site. Verifying the manufacturer's on-hand orders, bottleneck equipment, key materials and test bench schedules is closer to the true delivery risk than looking at theoretical annual capacity.
Before signing the contract, put the most difficult set of operating conditions back into the technical agreement, requiring the candidate to explain the design basis, verification method and interface responsibility. Manufacturers who are able to clarify these issues one by one and leave verifiable evidence are truly within the scope of comparability.